+84 28 3820 8888
Technical information and applications.
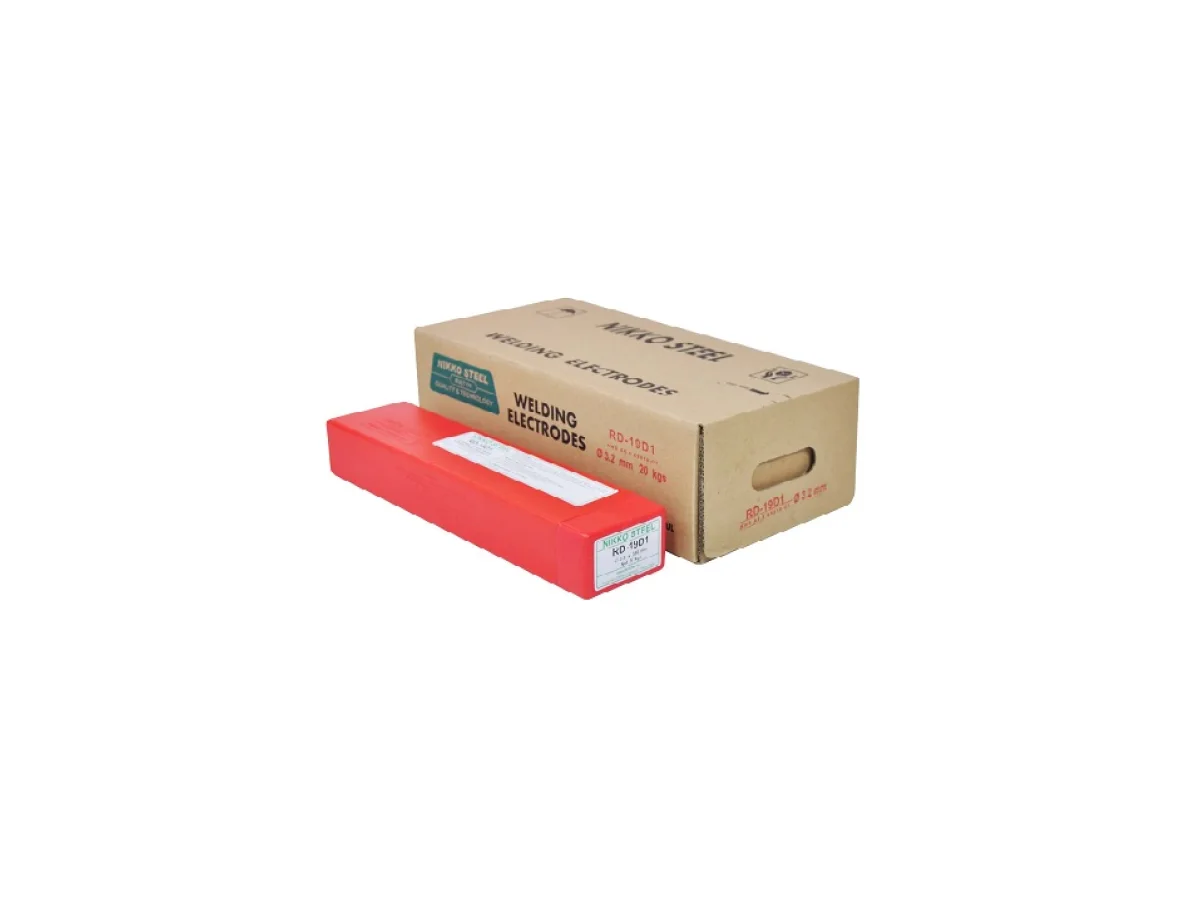
NIKKO Welding Electrode RD-19D1 belongs to the MMA Electrodes for High Tensile & Low Alloy Steels range. Confirm classification, base material, welding current and operating conditions before requesting a quotation.
CLASSIFICATION
AWS A5.5 E9018-D1 | EN ISO 18275-A E 55 4 ZMnMo B
PRODUCT DESCRIPTION
The design emphasis of the chemically basic flux is engineered to ensure the optimum weld metal properties demanded by the specification are fully met. The basic flux containing the appropriate alloying elements with a controlled balanced addition of iron power, is extruded onto a high purity ferritic core wire with a blend of silicates that ensures both coating strength and a coating resistant to subsequent moisture absorption.
WELDING FEATURES OF THE ELECTRODE
The chemical nature of the flux together with a significant proportion of iron powder ensures maximum deposition efficiency without detracting from its ability
to be used in all positions except vertical down. Overall the arc is very stable, slag detachability is good and metal recovery is some 115% with respect to the core wire
APPLICATIONS AND MATERIALS TO BE WELDED
Suitable for welding steels with a minimum UTS of 700 N/mm2 meeting the properties both as welded or after PWHT. Typical materials include ASTM A514 used for pressure vessels, bridges and offshore constructional work. The addition of Mo increases weld metal strength at elevated temperature and maintains UTS after PWHT and provides increased resistance to corrosion
OTHER DATA
Electrodes that have become damp should be re-dried at 150oC for 1 hour